A buyer sees two words on a quotation — “seamless” and “galvanized” — and it is easy to assume the product must be the safest choice. Not quite.
Those two features solve different problems. A seamless pipe removes the longitudinal weld seam from the pipe body. Galvanizing adds a zinc coating to help protect carbon steel against corrosion. Put them together and you have a useful product for certain projects, but you also have a more expensive specification that needs to be justified by the service conditions.
That distinction matters. Corrosion is not a small maintenance issue; AMPP reported in 2025 that the annual global cost of corrosion exceeds USD 2.5 trillion. But paying for a premium pipe construction where a compliant welded pipe would do the job is not good engineering either. The sensible question is not “Which pipe is best?” It is “Which combination of pipe construction, grade, wall thickness, coating and inspection fits the actual duty?”
Table of Contents
· What galvanized seamless steel pipe actually means
· Seamless versus welded: where the difference matters
· What hot-dip galvanizing adds
· A practical comparison for buyers
· What the galvanizing process can tell you about quality
· A real-world galvanized piping case
· What to put on an RFQ
· FAQ
What Galvanized Seamless Steel Pipe Actually Means
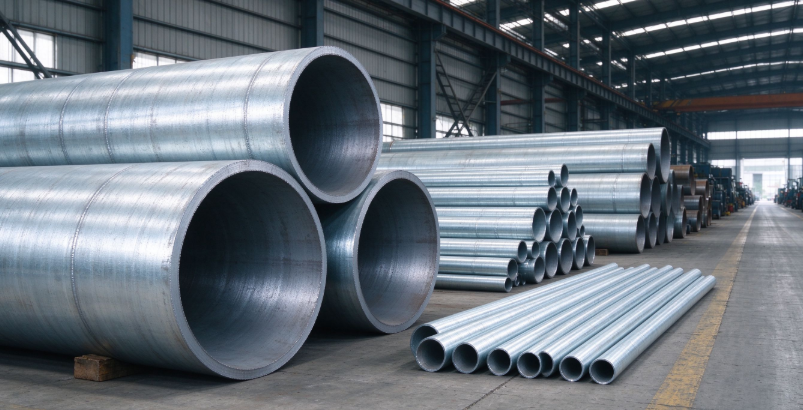
The product starts with seamless carbon steel pipe and then receives a zinc coating, typically by hot-dip galvanizing when durable corrosion protection is required. “Seamless” describes how the pipe body is made. “Galvanized” describes the surface protection. They are not grades, and they do not tell you the allowable pressure by themselves.
ASTM A53/A53M-24 is a useful reference because it explicitly covers black and hot-dipped zinc-coated steel pipe, including Type S seamless pipe in Grades A and B. Its scope runs from NPS 1/8 through NPS 26, and the standard covers pipe intended for mechanical and pressure applications as well as ordinary steam, water, gas and air lines. It also includes testing requirements such as tension, bend or flattening tests as applicable, hydrostatic testing and nondestructive electric testing.
That gives buyers a solid starting point. It does not mean every galvanized seamless pipe in the market is automatically ASTM A53 compliant. The order still needs to identify the standard, grade, dimensions, end finish, test requirements and coating condition.
The phrase “seamless is stronger” needs more care
I hear this shortcut a lot. Seamless pipe has no longitudinal weld seam, which can be valuable in applications where the design, code, purchaser specification or service conditions call for Type S pipe. But a properly manufactured welded pipe is not automatically a weak product. ASTM A53 itself covers seamless and welded types for mechanical and pressure service.
Pressure capability comes from the full specification: material grade, outside diameter, wall thickness, manufacturing route, heat treatment where required, testing and the governing design code. If a sales page tells you “seamless always handles higher pressure” without asking about those items, it is selling a slogan, not solving a piping problem.
What Hot-Dip Galvanizing Adds
Bare carbon steel needs a corrosion strategy when the environment can keep it wet, expose it to weather or subject it to repeated condensation. Hot-dip galvanizing protects steel in more than one way. The zinc coating acts as a barrier, zinc also provides sacrificial or cathodic protection to exposed steel at small damaged areas, and a zinc patina develops as the coating weathers.
For tubular products, one practical attraction is the possibility of protecting both the outside and the inside surfaces when the galvanizing process is designed for full coverage. That can be difficult to achieve later with field-applied paint, especially once a pipe system is assembled.
Still, zinc is not a universal chemical lining. A galvanized surface must be checked against the conveyed medium, operating temperature and project code. If the process fluid is aggressive to zinc, the correct answer may be a different coating, a lining, stainless steel or another material system. Surface protection should follow the service environment, not the catalog photo.
Galvanized Seamless vs. Other Common Choices
Decision Factor | Galvanized Seamless Pipe | Galvanized Welded Pipe | Black Seamless Pipe |
Pipe body | No longitudinal weld seam | Weld seam is present; performance depends on the applicable pipe standard and weld quality | No longitudinal weld seam |
Corrosion protection | Zinc coating plus steel substrate | Zinc coating plus steel substrate | No zinc coating unless another protection system is added |
Typical reason to specify | Seamless construction is required and exposed carbon steel also needs zinc protection | Zinc protection is needed and a compliant welded pipe is acceptable | Seamless construction is required but galvanizing is unnecessary or another coating will be used |
Purchase risk | Paying for seamless construction without a real design reason; vague coating requirement | Assuming “welded” means low quality instead of checking the standard | Forgetting the cost and access requirements of later corrosion protection |
What to verify | Pipe standard, grade, dimensions, tests, galvanizing route, coating acceptance | Same, plus welded pipe type and applicable seam requirements | Pipe standard, grade, tests and the separate corrosion-control system |
A useful procurement habit is to separate the decision into two lines. First: what pipe body does the design require? Second: what corrosion-control system does the environment require? Only after those answers line up should “galvanized seamless steel pipe” become the purchase description.
What the Galvanizing Process Can Tell You About Quality
Surface preparation does most of the quiet work in a galvanizing shop. Zinc will not bond properly to oil, heavy oxide or poorly cleaned steel. In our general steel-processing practice, the batch hot-dip galvanizing sequence is controlled through degreasing, pickling, rinsing, flux treatment and drying before immersion in molten zinc. A practical shop-floor reference in our process handbook uses a zinc-bath range of roughly 450–470°C, with immersion time adjusted to the workpiece and section thickness.
Here is the important caveat: those are general fabricated-steel process controls, not a blanket specification for every galvanized pipe line. ISO 1461:2022, for example, covers hot-dip galvanized coatings on fabricated iron and steel articles but specifically excludes tube and pipe hot-dip galvanized in automatic plants. For pipe, the product standard and the actual galvanizing route have to be checked together.
This is where experienced buyers separate a coating description from a coating specification.
Four things I would look at before discussing coating “beauty”
· Surface continuity. Bare areas, peeling, heavy runs or obvious missed coverage deserve attention before color uniformity does.
· Coating thickness. A magnetic coating-thickness gauge is a practical nondestructive inspection method for galvanized steel. The acceptance value should come from the applicable product or coating specification, not from a salesperson’s generic range.
· Traceability. Pipe heat or lot identity, base-pipe certificate, galvanizing batch and final inspection should remain connected. Once bundles are mixed, paperwork becomes much harder to trust.
· Ends and later fabrication. Threading, cutting, grooving or welding after galvanizing can locally remove or damage the zinc layer. The order should say what end processing is required and how affected areas will be handled.
Our internal quality-control routine follows the same basic logic used across steel processing: incoming material verification, first-piece confirmation when a new setup starts, in-process checks, final inspection and retention of traceable quality records. It is not glamorous, but it catches far more problems than a polished product photo.
Real-World Case: Utah Water Research Laboratory
The Utah Water Research Laboratory at Utah State University provides a useful example of why engineers sometimes choose hot-dip galvanized piping when water exposure and maintenance access matter. The American Galvanizers Association reports that the facility uses galvanized pipes to bring water into its testing systems. The main facility has gravity-flow capacity above 100,000 gallons per minute, while the newer facility has pumped capacity above 50,000 gallons per minute.
The project source says hot-dip galvanizing was selected for durability and because the pipe could be protected on the interior and exterior in one operation. The documented galvanized components included pipe, angle frame and plates, with 34 tons of steel in the project and 31 tons hot-dip galvanized.
One detail is worth stating plainly: the case study does not identify the pipe as seamless. I would not use it to claim that seamless construction caused the performance. What it does show is the engineering value of full zinc protection on piping where water exposure and future coating maintenance are real concerns. That is the kind of distinction technical content should make.
Where Galvanized Seamless Pipe Usually Earns Its Place
The combination starts to make sense when three conditions overlap.
The design has a real reason for seamless pipe
That reason may come from the project specification, pressure class, purchaser standard, forming requirement or a preference for Type S construction. If nobody can explain why seamless is needed, challenge the requirement before the purchase order is released.
Carbon steel still needs corrosion protection
Outdoor utility systems, exposed mechanical services, water-related installations and industrial structures can create persistent moisture exposure. Galvanizing can reduce dependence on field painting where the service environment is compatible with zinc.
Maintenance access is expensive or disruptive
A coating is more valuable when repainting means scaffolding, shutdowns, confined access or removal of adjacent equipment. The initial material price is only one line in the life-cycle cost.
That does not turn galvanized seamless pipe into a default choice for oil, gas, chemical or high-temperature service. Those applications are governed by specific design codes and media compatibility. A zinc coating should never be used to “upgrade” a base pipe that does not meet the underlying piping specification.
What to Put on the RFQ
A clean request for quotation saves more time than a week of clarification emails. At minimum, I would put the following items on the inquiry:
· Pipe standard and required type, for example ASTM A53/A53M Type S where applicable
· Grade
· NPS or outside diameter and wall thickness / schedule
· Length tolerance and quantity
· Plain, beveled, threaded, grooved or coupled ends
· Hot-dip galvanized or another clearly defined zinc-coating process
· Coating acceptance requirement and inspection method
· Required hydrostatic, NDE or mechanical test documentation
· Mill test certificate and traceability requirement
· Any post-galvanizing fabrication, marking, packing and export requirements
If a supplier quotes only “GI seamless pipe, standard export quality,” send it back. The phrase contains almost no engineering information.
FAQ
Is galvanized seamless steel pipe always better than galvanized welded pipe?
No. It is a different specification. If the project accepts a welded pipe manufactured and tested to the governing standard, seamless construction may add cost without adding useful value. Choose the pipe body first, then choose the corrosion protection.
Can ASTM A53 include galvanized seamless pipe?
Yes. ASTM A53/A53M-24 covers black and hot-dipped zinc-coated pipe and includes Type S seamless Grades A and B. The standard also defines size scope and test requirements. The purchase order still needs to state the specific type, grade and dimensions.
Should I use ISO 1461 as the only galvanizing requirement for pipe?
Not automatically. ISO 1461:2022 excludes tube and pipe hot-dip galvanized in automatic plants. If your pipe is galvanized on an automatic line, use the appropriate pipe/product requirement and confirm how coating acceptance is defined.
What is the fastest way to screen a galvanized seamless pipe supplier?
Ask for a sample MTC, the base-pipe standard, the galvanizing process route, coating inspection records and the lot-traceability method. A supplier that can answer those five points clearly usually gives you a much better starting position than one that leads with a zinc-coating number and a low price.
A Better Way to Buy It
Galvanized seamless steel pipe makes sense only when seamless construction and zinc protection each solve a real project need. Put the pipe standard, grade, size, wall thickness, service environment, end finish and coating requirement on the same RFQ. A competent supplier should then be able to confirm the fit — or recommend a simpler specification before you spend extra money.